The Chip You Bought and the Chip You Got: Understanding Semiconductor Grade Allocation
There is a quiet negotiation happening inside every semiconductor fabrication facility that most engineers never witness. Long before a chip reaches a distributor's catalog or lands on a purchasing manager's desk, it has already been evaluated, scored, and sorted into a hierarchy that will define its entire commercial life. That process — semiconductor binning — determines not just what a component is labeled, but what it is actually capable of delivering under real-world conditions. For engineers designing systems intended to operate reliably across temperature extremes, voltage fluctuations, or extended service lifetimes, understanding this hidden allocation logic is not optional. It is foundational.
The Same Die, Many Destinies
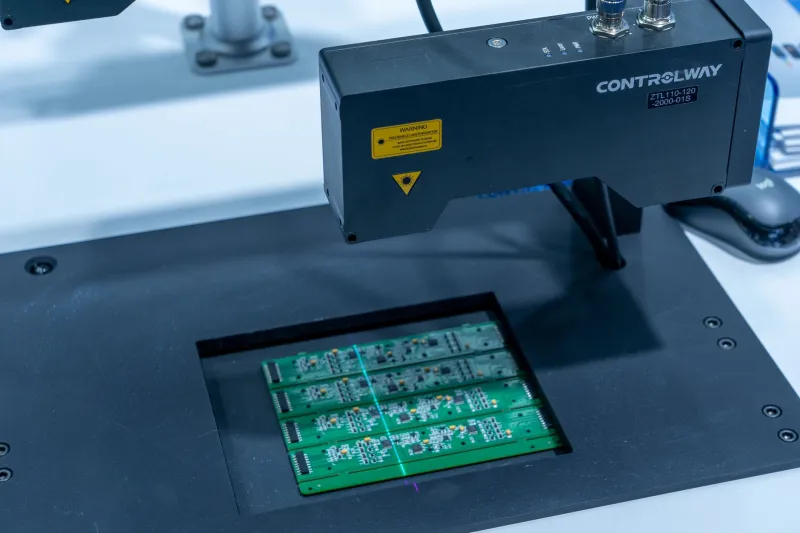
Modern semiconductor manufacturing produces wafers containing hundreds or thousands of individual dies, each fabricated under nominally identical conditions. In practice, however, process variation is unavoidable. Minute differences in dopant concentration, oxide thickness, lithographic alignment, and dozens of other physical parameters mean that no two dies perform identically. Automated test equipment probes each die while it is still on the wafer, measuring parameters such as maximum stable clock frequency, leakage current at specified voltages, noise characteristics, and threshold voltages.
The results of this testing feed into a binning algorithm that assigns each die to a performance tier. The highest-performing dies — those that meet every specification with margin to spare — are typically allocated to industrial, automotive, or military-grade product lines, where operating temperature ranges are wider and qualification standards are more demanding. Mid-tier dies become standard commercial components. The remainder, which may still meet a reduced specification set, are often sold into consumer markets under simplified part numbers or lower price points.
What makes this arrangement consequential for engineers is that the physical silicon in two differently graded parts may be structurally identical. The differentiation is imposed through testing thresholds, firmware locks, or simply the marketing designation stamped on the package.
Why Commercial-Grade Components Carry Hidden Ceilings
Consider a hypothetical microcontroller offered in both a commercial-temperature variant and an industrial-temperature variant. The commercial part is rated from 0°C to 70°C; the industrial variant carries a −40°C to 85°C rating. A naive reading of these specifications might suggest that the underlying silicon differs between them. In many cases, it does not. The industrial part is simply a die that tested well enough at temperature extremes to justify the broader rating. The commercial part may contain silicon that was never tested beyond the commercial window — or that failed to meet the tighter performance criteria at the boundary conditions.
This creates an uncomfortable scenario for engineers who deploy commercial-grade components in environments that occasionally drift outside the nominal temperature range. The component was never validated to perform there. Worse, there may be no visible failure mode — just subtle timing violations, elevated leakage, or marginally degraded noise immunity that manifests as intermittent system behavior. Debugging these failures is notoriously expensive, and the root cause is rarely traced back to a grade allocation decision made before the part ever left the foundry.
How Allocation Strategies Shift With Market Demand
The allocation of dies across market tiers is not static. It responds to commercial pressures in ways that can affect engineers who rely on consistent component behavior across production runs.
During periods of strong demand in the industrial or automotive sector, manufacturers may allocate a larger proportion of high-performing dies to those customers, leaving fewer for the commercial pool. The commercial-grade components produced during that period may contain dies that are clustered closer to the minimum passing threshold. Conversely, during demand downturns, commercial bins may temporarily receive dies that would otherwise have been upselected to premium grades.
This variability is rarely disclosed in datasheets. Manufacturers have little commercial incentive to advertise that the performance distribution within a given part number shifts with market conditions. For engineers building systems with long production lifetimes — defense electronics, medical instrumentation, industrial control systems — this creates a meaningful reliability risk that is difficult to quantify without access to test data that most suppliers treat as proprietary.
Reading Between the Lines of Qualification Documentation
Sophisticated procurement practices can partially mitigate exposure to grade allocation uncertainty. Military and aerospace programs have long required suppliers to provide lot-specific test data, including the actual measured values for critical parameters rather than simply confirmation that a part passed or failed. This practice, sometimes formalized through AEC-Q100 automotive qualification requirements or MIL-PRF standards, forces transparency about where a specific lot falls within the specified range.
For engineers outside those regulated industries, the practical equivalent is to request sample characterization data before committing to a component in a new design. Some distributors maintain application engineers who can facilitate this. Others will provide access to manufacturer characterization reports that reveal the statistical distribution of key parameters across a production lot.
Where that data is unavailable, conservative design practice demands treating commercial-grade specifications as genuine limits rather than comfortable guidelines. Designing circuits that function correctly only when a component performs at the upper end of its specified range is a strategy that invites failure as lot compositions shift.
The Upscreen Option and Its Costs
One approach taken by organizations with stringent reliability requirements is upscreening — purchasing commercial-grade components and subjecting them to additional testing to identify which units meet tighter criteria. A manufacturer might buy commercial-temperature microcontrollers and test them across the industrial temperature range, retaining only those that pass for use in demanding applications.
Upscreening is effective but expensive. It adds testing cost, introduces handling risk, and requires access to calibrated thermal chambers and automated test equipment that smaller engineering teams may not maintain in-house. Third-party upscreening services exist throughout the US market, primarily serving defense and aerospace customers, but the economics rarely make sense for consumer or commercial IoT applications.
The more practical lesson for most engineers is simply awareness. Knowing that the chip on your bill of materials was allocated to its market tier through a statistical process — not through any guarantee of individual performance — changes how you interpret its datasheet and how much margin you build into your design.
Designing With Allocation Reality in Mind
The most resilient response to semiconductor grade allocation uncertainty is a design philosophy that does not depend on components performing at or near their specified limits. Voltage regulators with genuine headroom, thermal designs that keep junction temperatures well below maximum ratings, and timing architectures that tolerate clock variation — these are not luxuries. They are the engineering equivalent of acknowledging that what you receive from your distributor may not be the best silicon the foundry produced that quarter.
For engineers specifying components in applications where field failure carries serious consequences, the conversation with the supply chain should begin long before the first prototype is assembled. Understanding how your chosen manufacturer bins its production, which markets receive priority allocation, and what qualification data is available for the specific lot you are purchasing is not excessive diligence. It is the minimum standard for designing systems that behave as intended across their entire service life — not just during the optimistic conditions of initial laboratory testing.