Cracked at the Joint: Why Solder Fatigue Quietly Destroys Products That Passed Every Test
A product clears every qualification hurdle. It survives thermal shock chambers, passes vibration tables, and ships to market with a clean certification record. Then, eighteen months into deployment, field returns begin accumulating. Boards arrive with no obvious damage—no burned components, no corroded traces—yet they simply stop working. A close inspection under a stereo microscope reveals the culprit: hairline fractures threading through solder joints that look, to the naked eye, perfectly intact.
This is solder joint fatigue, and it is one of the most underestimated failure mechanisms in electronics manufacturing today.
The Physics of a Joint Under Stress
Every time a circuit board powers on, it heats up. Every time it powers off, it cools down. That cycle sounds benign, but it imposes a relentless mechanical burden on every solder joint connecting a component to its pad. The reason is straightforward: different materials expand at different rates when heated. A ceramic capacitor body, a copper PCB pad, and the solder alloy bridging them each carry a distinct coefficient of thermal expansion (CTE). When temperatures rise, these materials attempt to grow by different amounts. The solder joint, sandwiched between them, absorbs the resulting shear stress.
Repeat that cycle thousands of times—as any consumer device will over a two- to five-year service life—and the accumulated plastic deformation inside the solder microstructure eventually nucleates microscopic cracks. Those cracks propagate incrementally with each subsequent cycle until electrical continuity is lost or resistance climbs high enough to cause intermittent failures that are notoriously difficult to diagnose.
The transition from leaded tin-lead solders to RoHS-compliant lead-free alloys, predominantly SAC305 (96.5% tin, 3% silver, 0.5% copper), has made this problem measurably worse. SAC305 is harder and less ductile than traditional 63/37 tin-lead. It accommodates plastic deformation less gracefully, meaning cracks initiate sooner under equivalent thermal loading. The tradeoff was necessary from an environmental and regulatory standpoint, but it shifted the burden onto design engineers who now need to be more deliberate about joint geometry, component placement, and thermal architecture.
Where Standard Testing Falls Short
Industry qualification standards—IPC-9701, JEDEC JESD22-A104, and similar documents—provide structured methodologies for evaluating solder joint reliability. These protocols are valuable, but they are not the same as predicting field performance.
Accelerated thermal cycling tests typically ramp boards between temperature extremes far more rapidly than any real-world environment would. The logic is sound: compress years of field exposure into weeks of testing by intensifying the stress. The problem is that the physics of solder fatigue are rate-dependent. Faster temperature ramps produce different stress distributions and crack propagation patterns than the slow, gradual cycles a device experiences sitting on a desk in an office that cools overnight. Accelerated tests generate data that can be extrapolated to field life estimates, but those extrapolations depend on empirical constants—Coffin-Manson fatigue parameters—that may not accurately represent the specific alloy, joint geometry, or substrate combination in a given design.
Vibration is another variable that qualification chambers struggle to replicate faithfully. A circuit board installed in an industrial enclosure mounted to a factory floor, or a consumer device dropped repeatedly into a bag alongside keys and charging cables, experiences a vibration spectrum that differs substantially from the sinusoidal or random vibration profiles used in standardized testing. Vibration-induced fatigue and thermal fatigue interact in ways that are additive and sometimes synergistic, accelerating crack growth beyond what either mechanism would produce in isolation.
Architectural Decisions That Actually Matter
Engineers who understand solder fatigue mechanics can build resilience into a design before a single board is assembled. Several decisions at the layout and component selection stage carry significant consequences.
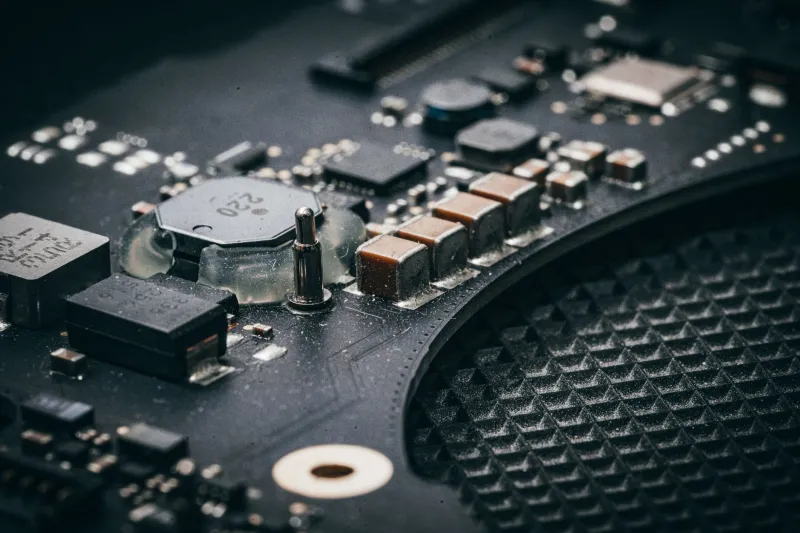
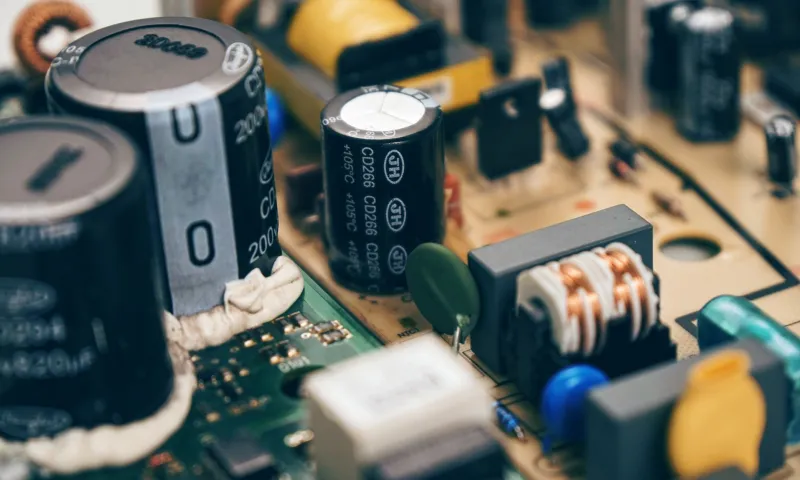
Component body size and standoff height directly influence how much shear displacement a joint must accommodate during a thermal cycle. Large ceramic capacitors—particularly those in 1210 or 2220 packages—are notorious fatigue initiators on boards that see wide temperature swings. Splitting a large capacitor into two smaller devices in parallel reduces the mechanical footprint and distributes the stress, often dramatically extending joint life without changing electrical performance.
Pad geometry and solder mask design affect how solder distributes across a joint and where stress concentrations form. Solder mask defined (SMD) pads constrain solder to a precise footprint but can create stress risers at pad edges. Non-solder-mask-defined (NSMD) pads allow solder to flow slightly onto the copper trace, producing a fillet that distributes load more gradually. For BGAs and large QFNs, underfill epoxy—applied after reflow to encapsulate the joint array—is one of the most effective interventions available, transferring a significant fraction of CTE mismatch stress from the solder into the epoxy matrix.
Board material selection is often treated as a cost decision but carries real reliability implications. Standard FR4 has a relatively high out-of-plane CTE, which stresses BGA joints severely during thermal cycling. Low-CTE laminates, ceramic substrates, or metal-core boards can reduce this mismatch, though at higher cost. For products destined for harsh environments, the material premium frequently justifies itself in warranty savings alone.
Thermal management at the system level is worth reconsidering specifically through the lens of joint fatigue. Reducing the delta-T a board experiences during a power cycle—by improving heat spreading, adding thermal mass, or managing power sequencing to slow warm-up rates—directly reduces the mechanical strain amplitude imposed on every joint. A board that runs consistently warm may actually accumulate less fatigue damage than one that swings widely between cold and hot.
Closing the Gap Between Lab and Field
The most honest acknowledgment an engineer can make is that no qualification test perfectly predicts the variety of abuse a product will encounter across millions of units deployed into unpredictable environments. What testing can do is characterize the dominant failure modes and establish confidence intervals around expected life.
Building that confidence requires treating solder joint fatigue as a first-class design constraint rather than a manufacturing concern to be addressed after the schematic is finalized. Finite element analysis (FEA) tools capable of modeling CTE mismatch and solder creep behavior have become increasingly accessible, and running a thermal stress simulation during the layout phase costs far less than a field recall.
For makers and smaller engineering teams without access to enterprise simulation software, the practical guidance is simpler: respect the known risk factors, avoid large ceramic packages in high-cycle applications, use underfill where joint arrays are dense, and design thermal management to minimize temperature swings rather than merely maximum temperature.
Solder joints are small, quiet, and invisible inside a finished product. They are also the physical foundation on which every circuit's reliability ultimately rests. Treating them as an afterthought is a decision that tends to surface, with considerable cost, somewhere between the warranty desk and the teardown report.